Service
How a job works
Checks, diagnosis and work on the point that stops the machine or the line. Every change stays traceable, with a backup of the previous version.
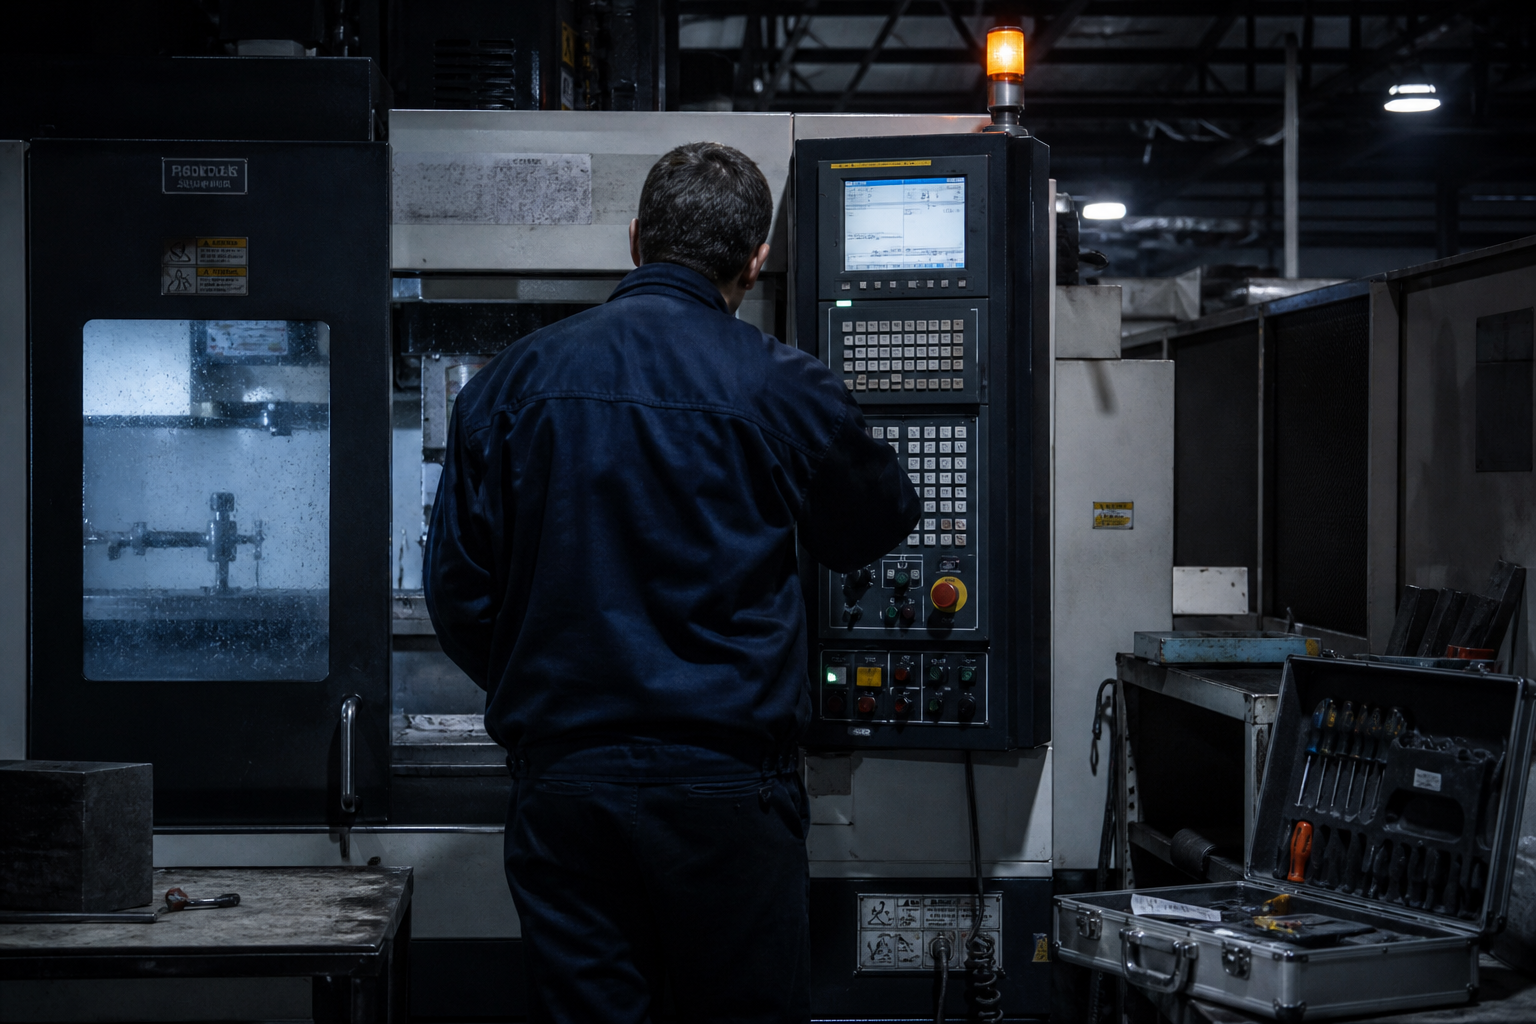
A machine can be technically running while the line stays down because of an interlock, a recipe or a program that is no longer aligned with the part. We intervene in a targeted way on the mechanics, the electrical system and the software, without reworking what is not causing the stop.
Before any change to the program we keep a backup of the previous version. At the end of the job the cycle, the safety functions and the handling have to be consistent again.
STEP 01
Request
Same working day
Email or the form. We need the machine model, the symptom and whether the line is down. The reply stays on the written channel.
STEP 02
Diagnosis / site visit
Within 24–48 working hours
Axes, spindle, electrical cabinet, PLC sequence and part program. We find the point that stops the cycle before replacing or rewriting what is not involved.
STEP 03
Intervention
Planned around the stop
Mechanical maintenance, wiring, or a targeted change to PLC, ISO and HMI. We keep a backup of the previous program and comment the changes.
STEP 04
Restart
End of intervention
Check of the cycle, the safety functions and the handling. The plant goes back into reliable production, with the previous version still recoverable.
Times below are indicative and confirmed when the job is taken on.